OCR and code reading
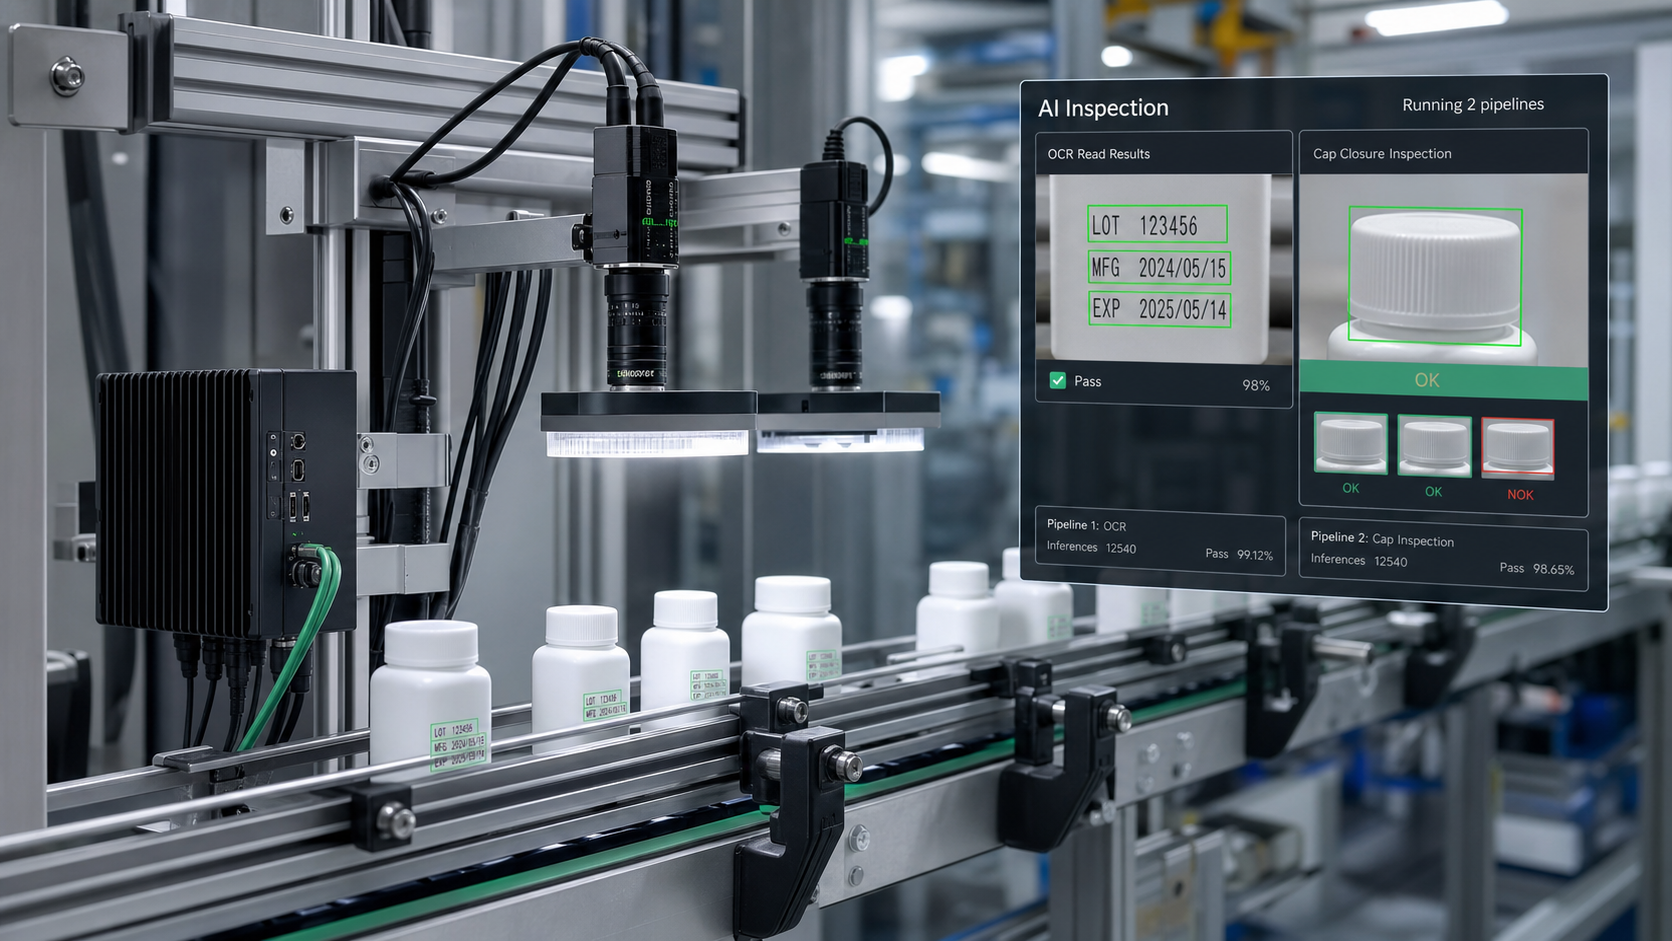
Detecting, reading and verifying values against recipes or print data.
Technology
We use the latest advances in machine vision to design solutions tailored to each customer’s individual needs.
What we offer
Detecting, reading and verifying values against recipes or print data.
Deep learning that detects hard-to-spot defects.
Results in milliseconds.
A broad selection of camera systems and optics from leading global manufacturers.
Diffuse, ring and line lighting tailored to individual requirements.
PLC, digital I/O, relays, ERP/MES and production data.
Tailored solutions
We design the system around your available space, line cycle time and inspection requirements.
Performance and compatibility
Simultaneous OCR/OCV processing, 1D/2D code validation, defect detection and packaging completeness inspection.
PLC communication, IT/OT convergence and ERP/MES connectivity.
 industrial cameras
 machine vision
 sensor intelligence
 sensors & vision
 industrial automation